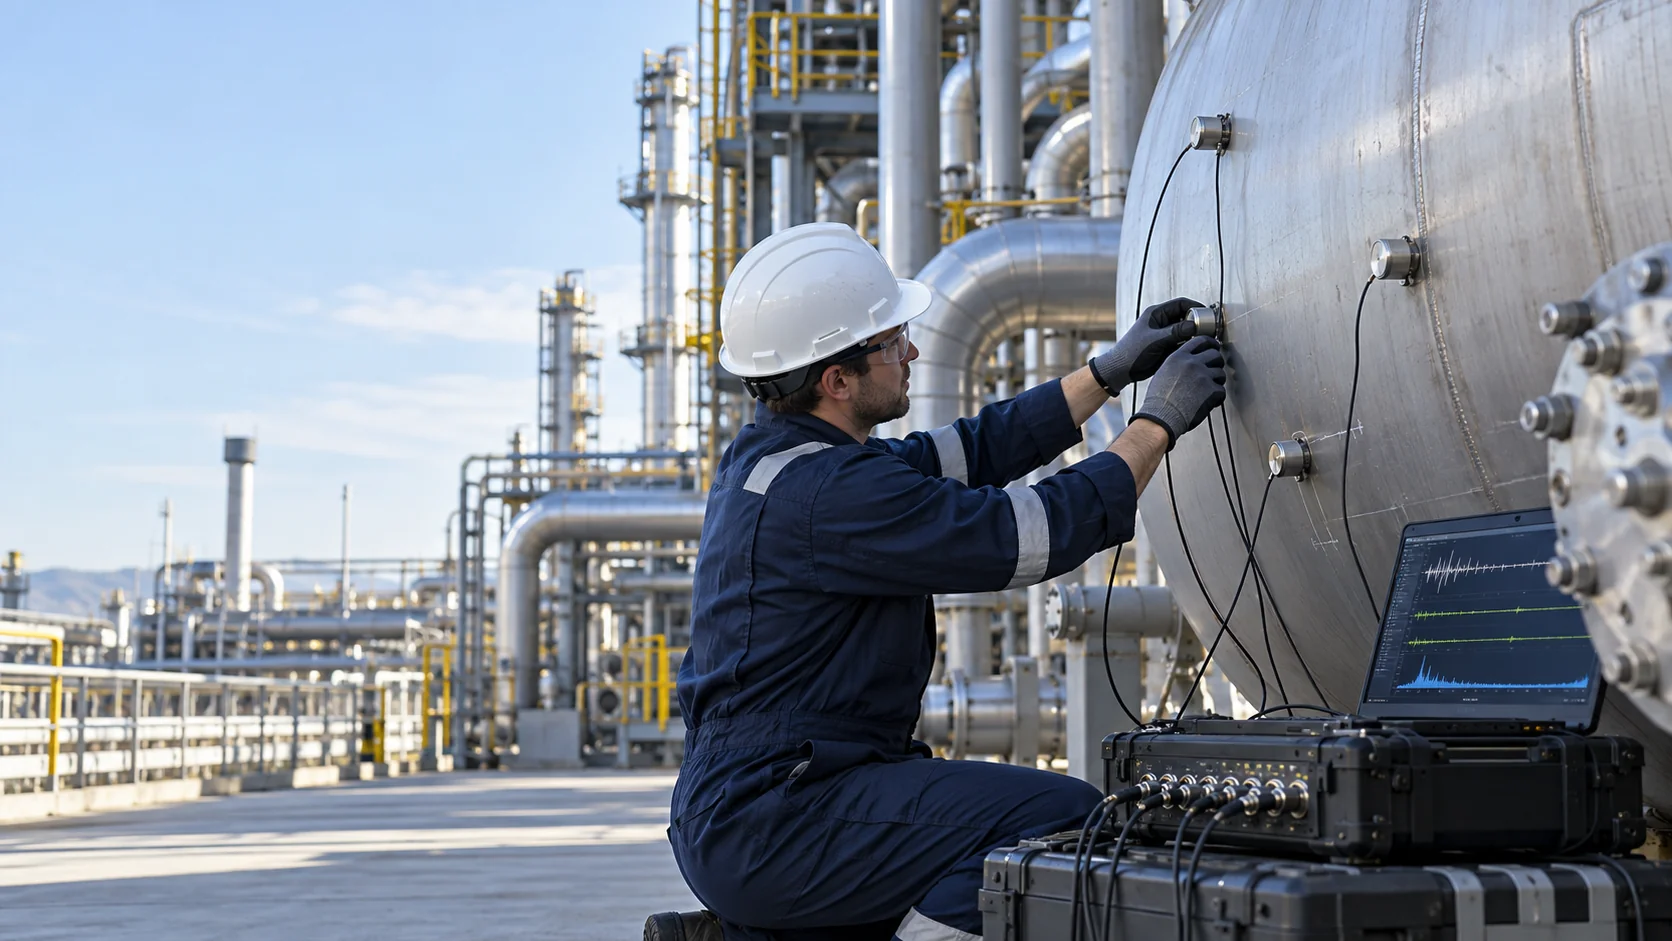
Geometry, material, access, loading and background noise are reviewed before scope confirmation.
Acoustic activity is interpreted together with the defined operating or loading condition.
Coverage, test record, quality checks and prioritized follow-up are documented clearly.
A project-specific service route
Pressure equipment AET begins with a defined question: Can the vessel be screened for active sources during a controlled pressure or loading cycle?
The service scope is developed from the asset drawing and history, the relevant material and geometry, site access, a safe loading or monitoring condition, and the decision required by the client. The agreed procedure identifies the applicable standard, monitored zones, instrumentation checks, data to retain and evaluation basis.
Typical candidate assets include reactors, separators, receivers, columns, autoclaves and other metallic pressure equipment. Feasibility and mobilization are confirmed for each enquiry.
What the inspection team would plan
1 · Pre-inspection review
Review the vessel code, pressure history, medium, safe test pressure, ramp and hold sequence, connections, temperature, surface access and acoustic noise. A depressurized or unchanging asset may not stimulate the suspected damage.
2 · Measurement setup
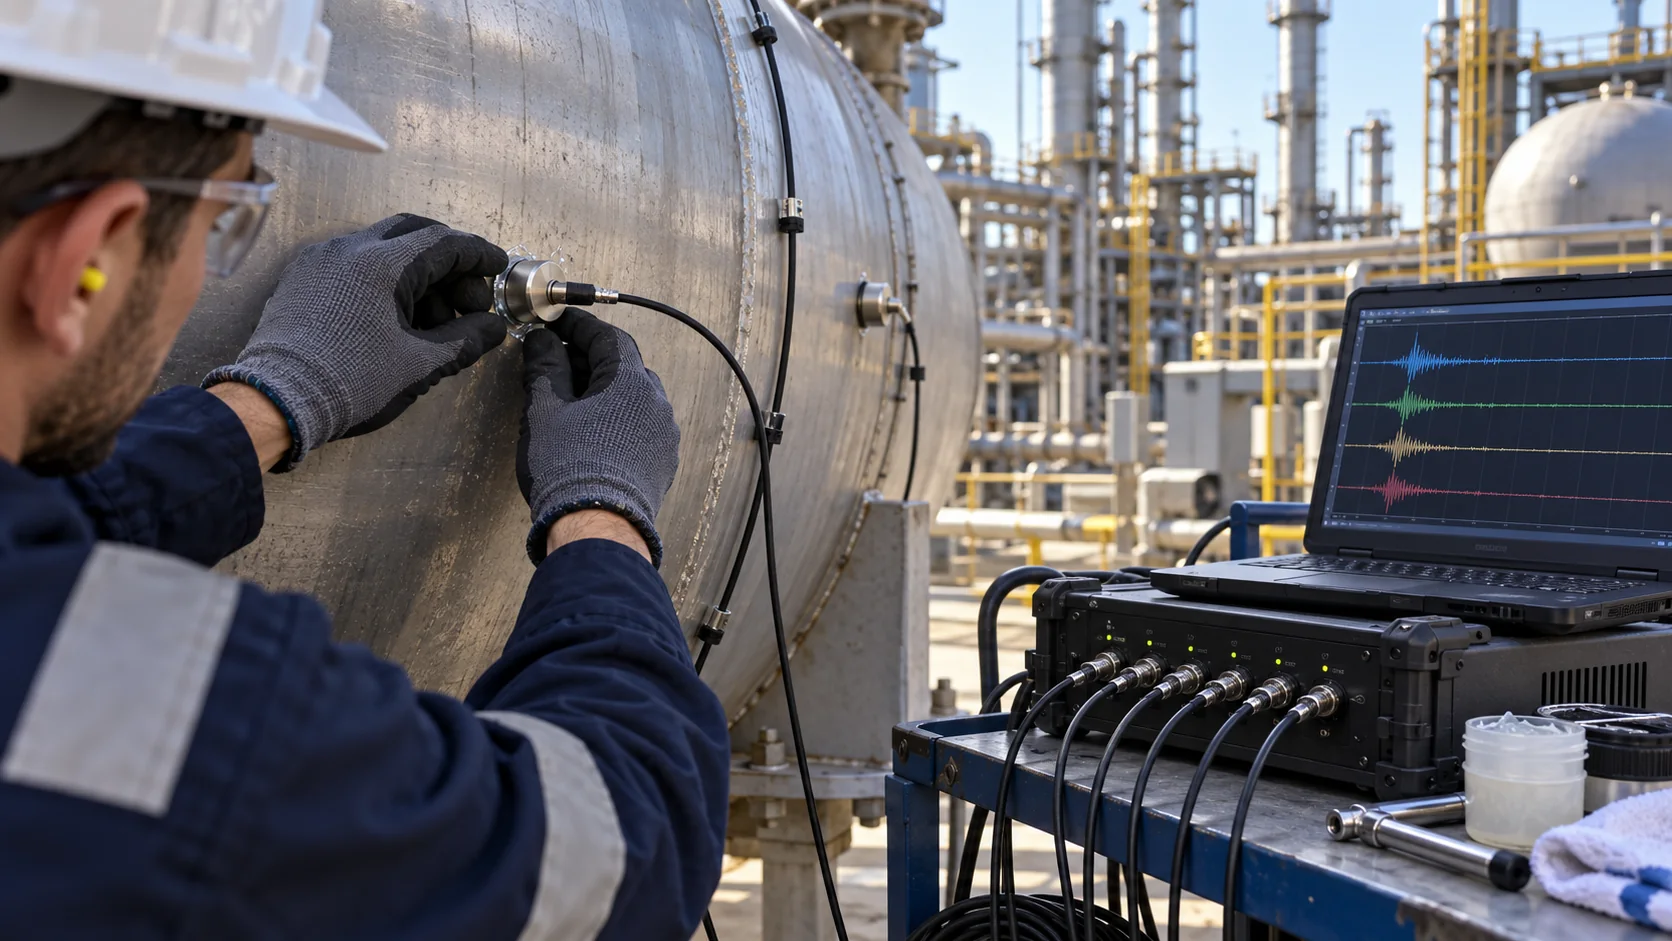
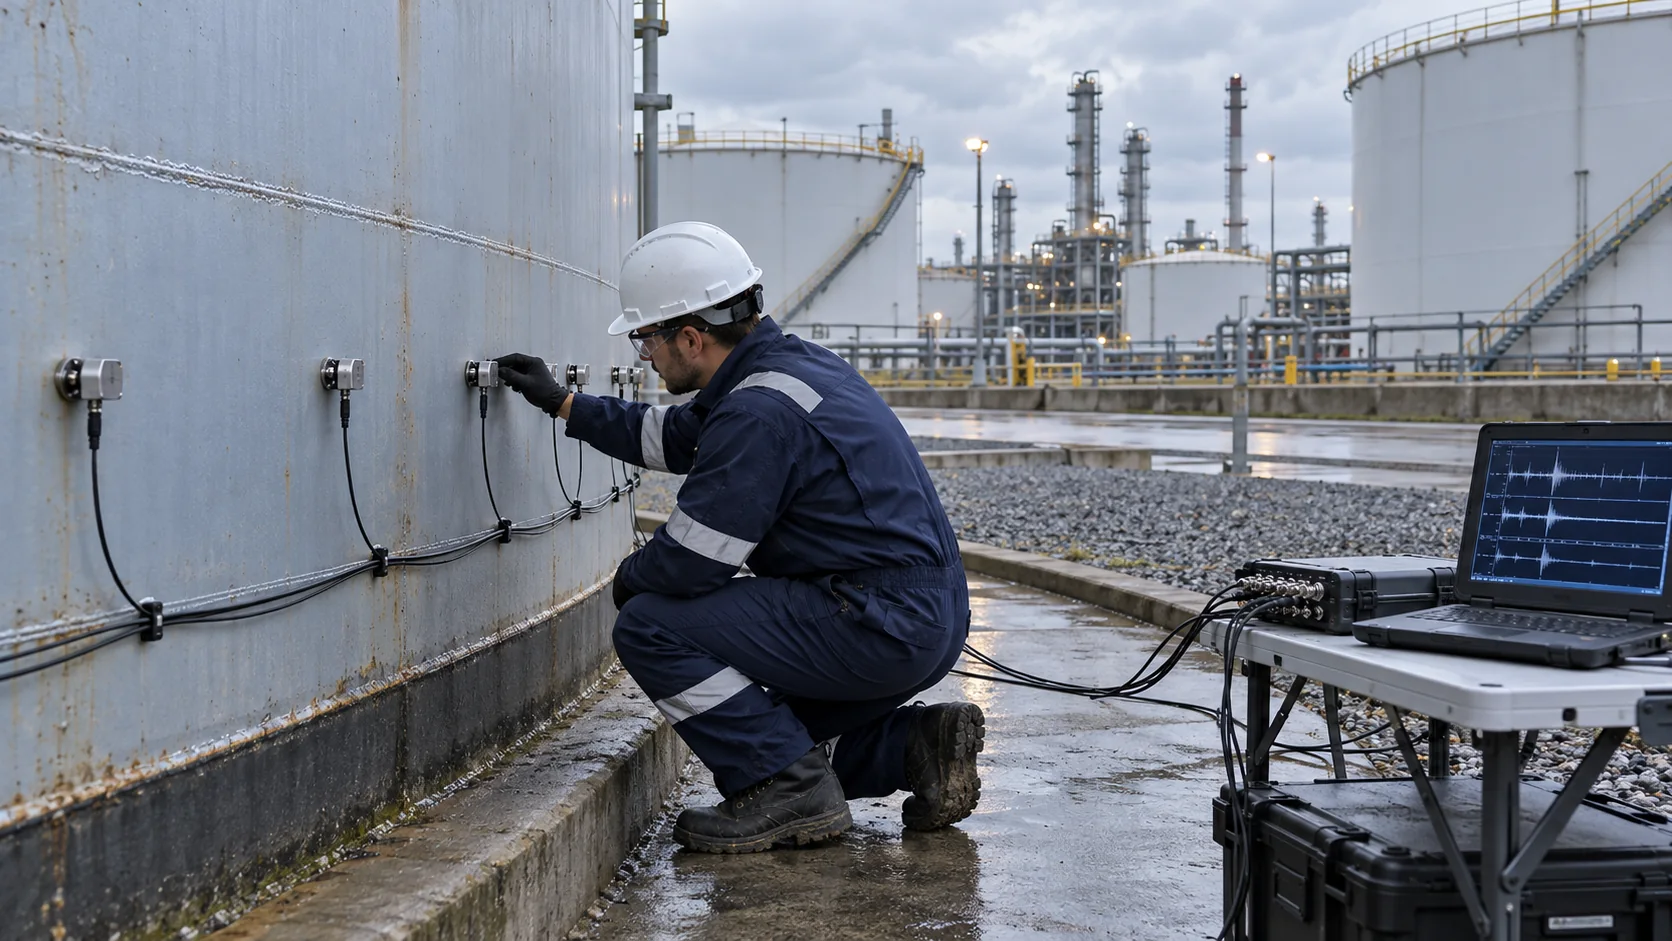
Document sensor locations and coupling; verify channels, timing, response and background noise. Record the stimulus alongside event data so the result can be interpreted in context.
3 · Data evaluation
Time-correlated activity, channel and source-location plots where localization is valid, loading history, quality checks and prioritized areas for follow-up.
4 · Targeted next step
Use targeted UT, PAUT, TOFD, surface examination or engineering assessment to characterize a localized area. AET cannot by itself size a crack or certify the whole vessel defect-free.
Scope and deliverables
A proposal should state the monitored boundary, site preparations, access and utilities, the pressure or operating sequence, applicable procedure and evaluation criteria. Reporting can include sensor layout, quality checks, loading history, event and location analysis where justified, an explicit coverage statement and recommendations for local examination.
AE responds to activity during the recorded condition. A silent interval cannot establish freedom from dormant defects; a located source is not a measured flaw size. A separate application guide explains how these limits apply to metallic pressure vessels.
Read the Metallic Pressure Vessels application guide → · Review the technical approach →
Acoustic emission testing in industrial environments
Sensor placement, test conditions and data acquisition are planned around the specific asset and inspection objective.
Discuss your inspection objective
Send the asset type, location, operating conditions and proposed loading or test window. We can review the information before defining a project-specific scope.